

Views: 283 Author: Weishi Sheets Publish Time: 2026-07-31 Origin: Site
Content Menu
● What Is a Glass Epoxy Sheet?
>> 1. Measure and mark the cut line
● Cutting Methods by Thickness
● Expert Tips for Better Results
● Industrial Applications and Real-World Use
● When to Choose a Supplier-Ready Cut Sheet
● FAQ
>> Can I cut glass epoxy sheet with a regular saw?
>> What is the safest way to cut FR4 board?
>> Can I use a utility knife on glass epoxy sheet?
>> How do I avoid chipping at the cut edge?
>> Is dust from cutting glass epoxy dangerous?
Glass epoxy sheet cutting looks simple, but the material behaves differently from wood, plastic, or metal. To achieve a clean edge, you need the right blade, stable support, dust control, and a method that matches the sheet thickness and final use.
Glass epoxy sheets are widely used in electrical insulation, industrial equipment, machining fixtures, molds, and structural parts because they combine mechanical strength, electrical insulation, and heat resistance. That is also why cutting them correctly matters: poor technique can cause chipping, edge splintering, delamination, and excessive dust.

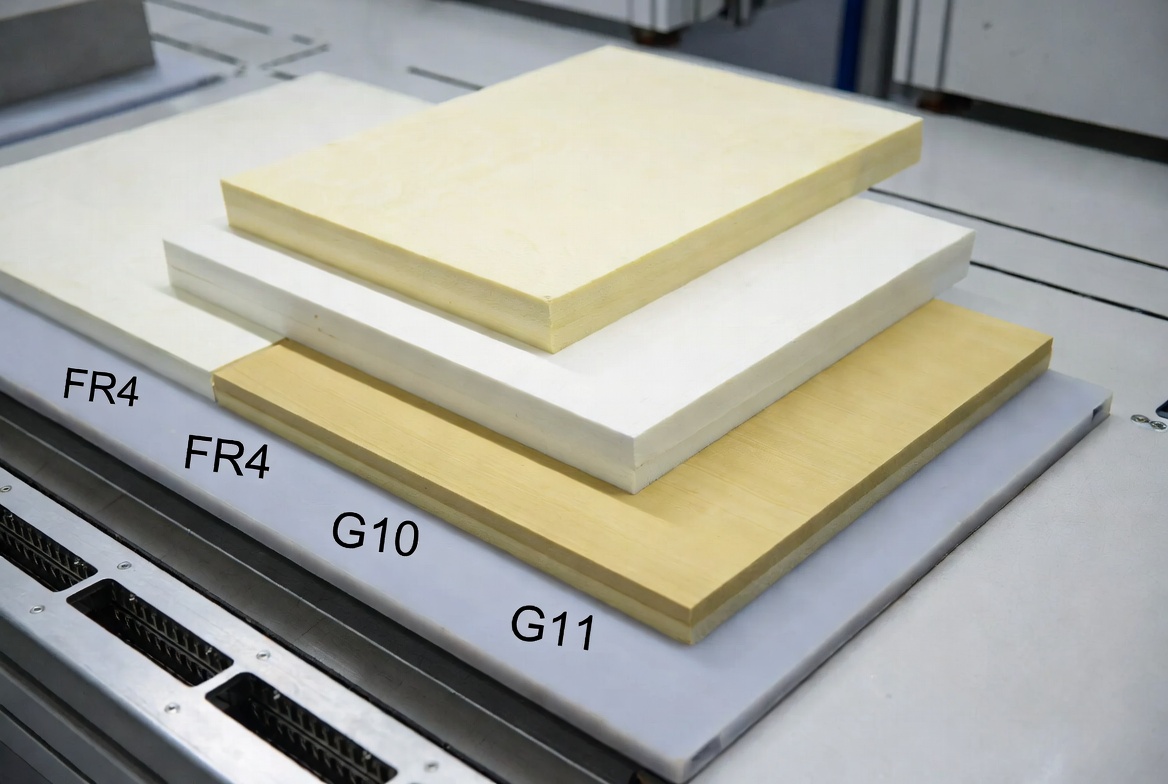
A glass epoxy sheet is a laminated composite made from fiberglass cloth and epoxy resin. In the market, it is commonly associated with FR4, G10, and G11 grades, each used for different temperature, insulation, and mechanical requirements.
These sheets are valued because they are rigid, dimensionally stable, and suitable for demanding industrial applications. However, the same layered structure that makes them strong also makes them abrasive and prone to edge damage if cut with the wrong tool.
Preparation is the difference between a clean cut and a ruined panel. Before any tool touches the sheet, measure carefully, mark clearly, and secure the material on a flat, stable surface.
Use the following checklist:
- Wear safety glasses, gloves, and a dust mask or respirator.
- Work in a well-ventilated area.
- Clamp the sheet firmly to reduce vibration.
- Use a clean, flat workbench.
- Prepare dust extraction or vacuum collection if possible.
A stable setup reduces flexing, which is especially important when cutting thinner sheets or precision parts. It also helps prevent chipping along the cut line.
Different tools are better for different sheet thicknesses and accuracy levels. The right choice depends on whether you need a straight cut, a detailed profile, or a production-grade finish.
| Tool | Best Use | Notes |
|---|---|---|
| Circular saw | Straight cuts on medium to thick sheets | Use a blade designed for composite materials |
| Bandsaw | General cutting and curved lines | Good control, but still needs dust control |
| Jigsaw | Small jobs and irregular cuts | Use a fine-toothed blade and cut slowly |
| Router | Edge trimming and shaped parts | Make multiple passes for cleaner results |
| Utility knife | Thin sheets only | Works for score-and-snap methods on thinner material |
For most industrial users, a saw with a composite-rated blade is the most practical choice. For thin sheets, scoring and snapping may work, but it is not ideal for thick or high-precision parts.
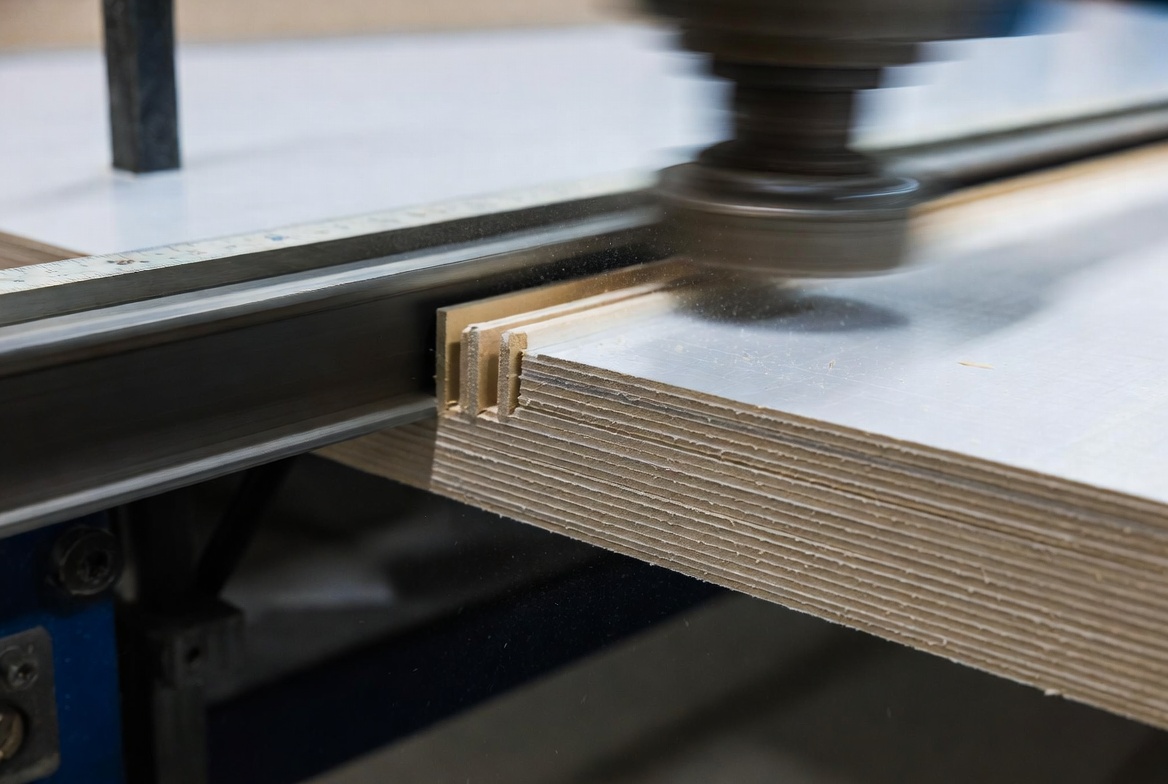
A controlled process gives the best finish and reduces waste. This method works well for FR4, G10, G11, and similar glass epoxy laminates.
Use a ruler, square, and fine marker to mark the cutting path clearly. Double-check the dimensions before cutting because composite sheets are harder to correct after the fact.
Clamp the sheet so it cannot move or vibrate during the cut. Even small movement can cause chipping or edge wandering.
Use a blade made for fiberglass, laminate, or composite material. Standard wood blades wear quickly and can leave rough edges.
Keep feed pressure steady and avoid forcing the tool. Slow cutting helps reduce heat build-up and lowers the risk of delamination or cracking.
After cutting, sand the edge with fine-grit sandpaper to remove burrs and sharp fibers. Clean the area thoroughly to remove dust and debris.
The best cutting method changes with thickness. Thin sheets can sometimes be scored and snapped, while thick industrial sheets usually require power tools.
- Thin sheets: score-and-snap or fine-tooth saw.
- Medium sheets: circular saw or bandsaw.
- Thick sheets: router, bandsaw, or industrial CNC process.
- Precision parts: CNC routing with controlled feed and dust extraction.
This matters because thicker boards resist clean snapping and are more likely to chip if the tool is too aggressive. In industrial environments, CNC-based cutting is often preferred when repeatability and edge quality are critical.
Many cutting problems come from small process errors. If you avoid the following mistakes, you can improve both safety and part quality.
- Using a blade not designed for composite material.
- Cutting too fast and overheating the sheet.
- Failing to clamp the board properly.
- Ignoring dust collection.
- Skipping edge finishing after the cut.
Overheating can damage the resin matrix and weaken the edge. Excess vibration can also create micro-chipping that becomes visible in final assembly or machining.
Industry practice shows that the cleanest results come from combining the right blade with controlled speed and proper support. For G10-type laminate cutting, a steady feed and dust extraction improve both safety and surface quality.
Here are three practical tips:
1. Use a fresh blade whenever possible, because dull blades increase chipping and dust.
2. Cut in one direction with support so the sheet edge does not break unpredictably.
3. Test on a scrap piece first when working with a new thickness, resin level, or tool setup.
For high-volume production, precision cutting should be standardized with consistent clamp pressure, cutting speed, and post-cut inspection. That approach improves repeatability and reduces scrap.
Not every glass epoxy sheet behaves the same way. FR4, G10, and G11 are related materials, but their performance can differ in heat resistance, mechanical properties, and application suitability.
That means your cutting method should reflect the material grade and the end-use requirements. For example, a part for electrical insulation may prioritize edge integrity and dielectric reliability, while a machining fixture may prioritize dimensional accuracy and surface finish.
Glass epoxy sheet is often used in electrical switchgear, PCB-related parts, machine jigs, insulating spacers, and industrial fixtures. Because these parts are frequently cut to exact dimensions, a controlled cutting process is not optional — it is part of product quality.
A practical example: a fabrication shop cutting insulating spacers for electrical cabinets may use a bandsaw for rough sizing, then a router for final trimming. This combination helps balance speed, precision, and edge quality.
Fiberglass dust is a serious concern during cutting and machining. Work in a ventilated area, wear protective equipment, and use dust extraction whenever possible.
Recommended safety gear includes:
- Safety glasses.
- Dust mask or respirator.
- Work gloves.
- Long sleeves.
- Hearing protection when using power tools.
A clean workspace is not just safer. It also makes inspection easier because dust buildup can hide edge defects or contamination.
If your project requires exact dimensions, tight tolerances, or repeated production runs, buying pre-cut or professionally machined glass epoxy sheet may be more efficient than cutting in-house. This is especially useful when your team lacks the right blades, extraction system, or machining setup.
For manufacturers, the best workflow is often to match the sheet grade, thickness, and machining method before production begins. That reduces waste and improves the consistency of final parts.
Yes, but a regular saw blade is not ideal. A blade designed for composite or fiberglass materials gives cleaner edges and reduces wear.
The safest method is to clamp the sheet firmly, wear protective gear, use dust extraction, and cut slowly with a composite-rated blade.
Only on thinner sheets. Score-and-snap methods are more suitable for thin material and are not recommended for thicker industrial boards.
Use a sharp blade, slow feed rate, proper clamping, and edge sanding after cutting. Chipping usually increases when the sheet vibrates or the blade is dull.
Yes. Fiberglass and resin dust should be controlled with ventilation, a respirator or dust mask, and vacuum extraction.
1. [JingHong — How to cut a FR4 sheet?] [jhd-material]
2. [JingHong — How to cut glass epoxy sheet?] [jhd-material]
3. [JingHong — How do you cut and machine FR4 epoxy resin sheets?] [jhd-material]
4. [JingHong — How to Cut and Machine Epoxy Glass Fiber Sheets Safely?] [jhd-material]
5. [Ztelecgroup — How to cut an epoxy fiberglass sheet?] [ztelecgroup]
6. [JingHong — Best Feeds and Speeds for CNC Cutting G10 Fiberglass Laminates] [blog.jhd-material]


